Manufacturing Built Around Your Brand Scale.
Flexible, cleanroom-grade contract manufacturing from pilot batch R&D trials to multi-ton commercial dry blending, milling, drying, and retail packaging.
Scale Your Formulations Without Heavy Capex Investment.
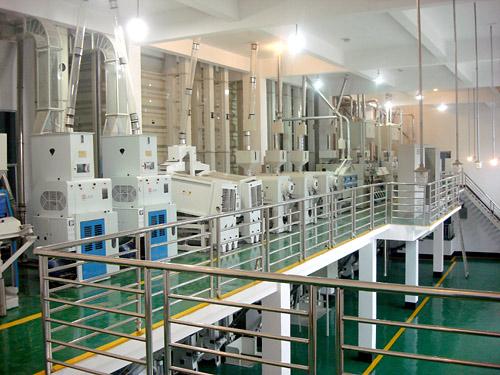
AAGAMAA serves as your specialized manufacturing partner. We eliminate production bottlenecks by providing certified cleanroom blending, cryogenic milling, liquid-on-powder infusion, and automated retail co-packing under one roof.
Whether launching a brand-new superfood blend, scaling an ancient grain bakery premix, or toll-processing botanical extracts for global export, our facility adheres to strict international hygiene and zero-allergen standards.
Comprehensive Contract Capabilities
Precision engineering and specialized food processing technologies tailored for consumer brands, retail chains, and industrial formulators.
Custom Blending & Homogenization
High-uniformity ribbon and paddle blending for functional beverage premixes, bakery dry blends, superfood powders, and micro-nutrient fortifications.
- Zero-cross-contamination lines
- Liquid-on-powder injection
- Homogeneity CV < 3%
Precision Milling & Particle Sizing
Low-temperature cryogenic milling, hammer mills, pin mills, and cyclone classification for standardized mesh sizes (30 to 200+ mesh).
- Sub-micron ultra-fine grinding
- Heat-sensitive botanical milling
- Multi-deck ultrasonic sieving
Advanced Drying Technologies
Spray drying, vacuum belt dehydration, and low-temperature fluidized bed drying for soluble extracts, fruit powders, and botanical concentrates.
- Carrier-free spray drying
- Preserved bioactive phyto-nutrients
- Controlled moisture < 4%
Botanical & Oleoresin Extraction
Supercritical fluid and solvent extraction for standardized curcuminoids, capsaicin, floral hydrosols, and food-grade essential oils.
- Standardized active assay
- Solvent-free residue protocols
- Pharma & food grade
Automated Packaging & Private Labeling
Turnkey retail packaging: stand-up zipper pouches, nitrogen-flushed pillow bags, bulk bag-in-box, hermetic tins, and biodegradable pyramid tea bags.
- Nitrogen gas flushing (Residual O2 < 1%)
- Multi-head rotary pouch packing
- Full barcode & batch serialization
In-Line Quality Assurance & Audits
Continuous quality control protocols with in-line metal detection, X-ray inspection, checkweighing, and third-party laboratory batch release.
- FSSC 22000 & HACCP standards
- Complete batch genealogy & COAs
- Zero-allergen cleanroom zoning
From Bench Prototype to Full Production
A disciplined 4-stage scale-up pipeline ensuring recipe stability, yield efficiency, and consistent consumer experience.
Bench Formulation & Feasibility
Lab-scale sample batches (1kg – 10kg), solubility characterization, rheology testing, and raw material sourcing verification.
Pilot Trial & Stability Audit
Pilot production run (50kg – 200kg), sensory evaluation, moisture testing, packaging compatibility, and shelf-life acceleration.
Commercial Scale-Up
Full commercial batch runs (1 metric ton to multi-container volume) with automated in-line mixing, sifting, and nitrogen packaging.
Quality Release & Global Dispatch
Multi-tier lab release (HPLC, microbial assay, heavy metals), COA issuance, palletization, and export freight handover.
Ready to Schedule a Pilot Run or Contract Batch?
Speak directly with our plant operations head and formulation team to evaluate line compatibility, packaging dies, minimum order quantities (MOQs), and production schedules.
Direct Plant Inquiries
Submit target batch volumes, raw material specs, or desired packaging formats for an immediate feasibility check.
We Also Design & Commission Complete Processing Plants.
From factory layout and automation to machinery sourcing and commercial handover.